Best Plunge Router Bits for Clean, Accurate Cuts
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
Contents
The best plunge router bits for clean, accurate cuts
For most plunge-routing in hardwood or plywood, choose a sharp, carbide-tipped, 1/2-inch-shank spiral bit with a cutting length just long enough for the cut; use a downcut spiral for a clean top edge, an upcut spiral when chip removal matters, or a straight bit for economical, shallow grooves. The best plunge router bits depend less on a “best overall” label than on stock thickness, cut depth, edge-finish needs, and the collet your router accepts.
One important distinction: a bit must be designed to plunge. Spiral bits and straight bits with cutting edges that extend to the center can enter material vertically. A standard edge-cutting pattern bit or many roundover bits cannot. Check the manufacturer’s specifications rather than assuming any bit that fits the collet is plunge-capable.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.
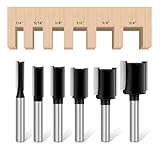


Choose by cut and material
| Cut or situation | Useful bit profile | Typical size to consider | Best fit |
|---|---|---|---|
| Clean groove in plywood or veneered stock | Downcut spiral | 1/4 in. diameter; 1/2 in. cutting length | Reduces tear-out on the top face; use shallow passes to manage chips |
| Deep mortise or slot in hardwood | Upcut spiral | 3/8 in. diameter; 1 in. cutting length | Lifts chips out of the cut; may leave a rougher top edge |
| General-purpose shallow dado or recess | Two-flute straight bit | 1/2 in. diameter; 3/4 in. cutting length | Lower-cost option for routine cuts with suitable chip clearance |
| Clean top and bottom faces | Compression spiral | 1/2 in. diameter; cutting length matched to stock | Can help limit tear-out on both faces when the cut spans the bit’s opposing flute sections |
| Small detail or narrow slot | Small-diameter spiral | 1/8–1/4 in. diameter | Fine features; use light passes because slender cutters are easier to deflect or break |
These dimensions are common buying reference points, not universal recommendations. Confirm the bit’s maximum speed, cutting length, total length, and plunge capability with its maker. A long cutting edge does not mean you should remove the full depth in one pass.
What matters when comparing bits
Profile: straight, upcut, downcut, or compression
A straight bit is often the practical choice for shallow dados, hinge recesses, and general routing. It usually costs less than a spiral and can work well when the router can clear chips and the cut is not especially demanding. In a deep, narrow slot, however, packed chips can cause heat, burning, or a poor finish.
An upcut spiral pulls chips toward the router, which helps clear a mortise or deep slot. Its tradeoff is that it can lift fibers at the top surface. A downcut spiral presses fibers toward the work, improving the top edge on veneer and laminate, but chips can collect in the cut. Keep the passes shallow and clear debris between passes.
A compression bit combines upcut and downcut sections. It is useful for through-cuts in sheet goods when both faces need a clean edge, provided the material thickness and cut depth engage the appropriate parts of the cutter. For a shallow plunge that uses only one section, it may not deliver the expected two-sided finish.
Cutting length and diameter
Match cutting length to the depth of the cut—not simply to the thickness of the board. Leave enough flute length for the planned pass, while avoiding an unnecessarily long cutter that can increase vibration and deflection. For a deep recess, reach the final depth through several passes rather than relying on the bit’s full cutting length at once.
Diameter affects both the shape and the load. A larger bit removes more material and needs a router and setup suited to its size; a smaller bit fits narrow details but is more vulnerable to bending. For a curved or narrow plunge cut, check that the bit diameter fits the path and that the router base remains supported throughout.
Shank: 1/4 inch or 1/2 inch?
Use a shank that matches the router’s collet exactly. A 1/2-inch shank generally offers greater stiffness than a 1/4-inch shank of otherwise similar design, which is helpful for larger cutters, deeper cuts, and frequent work. It is not automatically the right choice if your router only accepts 1/4-inch shanks. Never improvise with a mismatched collet or reducer unless the router and accessory makers specifically approve that setup.
If you are searching for the best 1/4 inch router bits, prioritize small cutters for light-duty detail work, short cutting lengths, and a quality carbide edge. A 1/4-inch shank is convenient and widely useful, but it is not the preferred substitute for a stiffer 1/2-inch setup on a large or heavily loaded bit.
Quick decision guide
| Your situation | Consider | Why |
|---|---|---|
| Occasional shallow grooves; keeping cost down | Carbide-tipped straight bit, correct shank, short cutting length | A straightforward, economical choice for basic work |
| Regular hardwood mortises | Carbide spiral upcut, preferably 1/2-inch shank if compatible | Chip lifting and added stiffness can help with deeper routing |
| Veneered plywood or a delicate top face | Downcut spiral for shallow grooves; compression bit for suitable through-cuts | Choose the profile around which face needs protection |
| New to plunge routing | Short, moderate-diameter bit and multiple shallow passes | Less demanding than a long, narrow cutter taking a deep bite |
| Only a 1/4-inch collet available | Small-diameter bit intended for that collet | Works within the router’s actual capacity; avoid oversized cutters |
Setup for a cleaner plunge cut
- Check the stock and layout. Mark the cut and secure the workpiece. On sheet goods, test the bit and feed direction on scrap from the same material.
- Set a modest depth per pass. For example, a 3/4-inch-deep mortise can be routed in three passes of about 1/4 inch each. Reduce the increment if the bit is small, the wood is dense, or the router sounds strained.
- Set the plunge stop and speed. Follow the bit maker’s maximum speed guidance; larger diameters typically require lower speeds. Make sure the bit is seated securely without bottoming out in the collet.
- Manage chips and support. Clear debris between passes, especially with downcut or straight bits. Keep the router base flat and stable; use a guide or fence when the cut needs a straight boundary.
- Make a test cut. Check depth, fit, and edge quality in scrap before routing the finished piece. A test also reveals whether the chosen profile leaves fibers that need a scoring pass or different bit.
Carbide, wear, and ownership
Carbide-tipped and solid-carbide bits hold an edge longer than basic high-speed-steel cutters in many woodworking applications, but they cost more and can chip if dropped or fed aggressively. Carbide-tipped bits are common for general-purpose use; solid-carbide spirals are often chosen for demanding, precise cuts, particularly in sheet goods and production work. Neither material excuses overheating or dullness.
Watch for burning, fuzzy edges, increased feed effort, or a cut that no longer matches the test result. These can indicate a dirty or dull edge, poor chip evacuation, an unsuitable feed rate, or a bit that has loosened. Resin and pitch buildup can also reduce cutting performance: use a cleaner intended for router bits, follow its directions, and dry the bit before storage. Avoid scraping carbide edges with hard tools.
Store bits so their edges cannot knock against one another. Replace a bit with chipped carbide or a damaged shank rather than trying to compensate with a slower feed. For the best router bits for plunge cuts, the right profile and sound condition matter as much as the initial purchase: a clean, correctly sized cutter used in controlled passes is more reliable than an oversized bit forced through a deep cut.