How to Align a Drill Press Table with the Spindle
What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
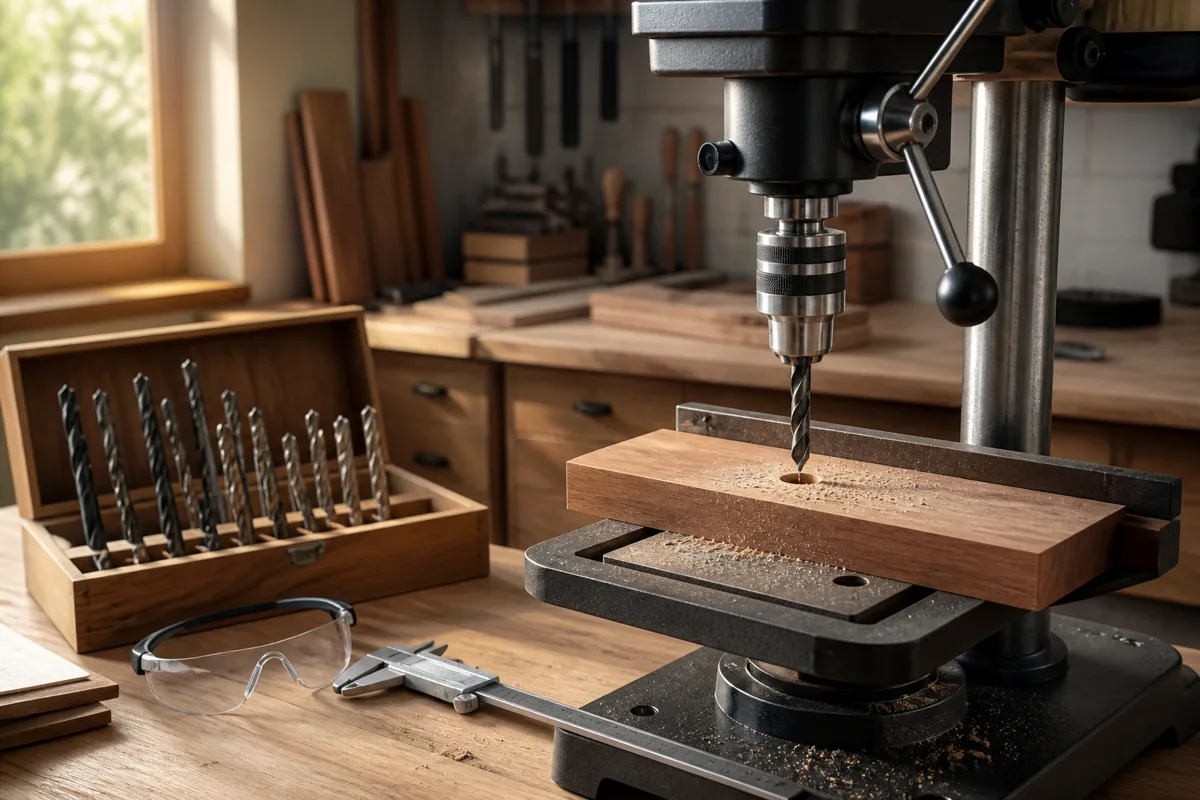
Aligning a drill press table means making its work surface square to the spindle, so a bit travels perpendicular to the table. That matters when drilling holes through a board, boring for hardware, or making matching parts. A table that tilts just a degree or two can leave a visibly angled hole, especially through thick stock.
Contents
What you need
Check your drill press manual first. Some machines have a table-tilt scale or a locking mechanism that must be loosened in a particular order. You’ll need a reliable square, a straight rod or known-straight drill shank, and a way to lock the table after adjustment. A machinist’s square gives more confidence than a small combination square, but a decent combination square is usually enough for furniture and shop work.
A drill rod or straight shank is preferable to a twist drill bit: the flutes can make a bit awkward to compare against a square. A ground steel rod is a useful purchase if you check alignment often; for occasional adjustment, a straight, undamaged shank may do. Compare options for a drill press alignment rod if you need one.
Check the machine before adjusting
Unplug the drill press. Raise the table enough to work comfortably, then remove any workpiece or accessory that might interfere. Clean sawdust and chips from the table, column, and tilt joint. Debris trapped between the table and its support can prevent a repeatable adjustment.
Bring the quill down and check that the spindle itself does not have obvious side play. Hold the rod near its lower end and gently push it sideways. A small amount of movement in the quill bearings can make your reading vary, and no table adjustment will fix worn or loose bearings. Also make sure the rod is seated straight in the chuck. Roll it on a flat surface if you suspect it is bent.
Set the table square to the spindle
Chuck the straight rod with enough length exposed to reach the table, then lower the quill until the rod is close to the surface without touching it. Put the square’s base flat on the table and bring its blade alongside the rod. Check the gap near the table and again higher up. The rod should be parallel to the square blade, with no visible wedge-shaped gap.
Check in two directions, roughly 90 degrees apart. A table can look square from the front while still being twisted relative to the spindle. Rotate the spindle by hand and watch the rod against the square. If the rod swings noticeably, it may be bent or poorly seated; correct that before moving the table. Do not run the motor while the square is beside the rod.
If the table tilts, loosen its tilt lock just enough to move it. Adjust until the rod and square agree in both directions, then tighten the lock gradually while watching for movement. Tightening can pull the table out of position, so recheck after locking. If the table has a scale, treat it as a rough reference, not a precision measurement.
Choosing a checking tool
| Tool | Best for | Trade-off |
|---|---|---|
| Combination square | Occasional setup and general shop work | Affordable and versatile; blade accuracy and short reach vary. |
| Machinist’s square | More repeatable checks on small or medium tables | Usually more rigid, but costs more and does less general measuring. |
| Dial indicator and sweep arm | Quantifying table variation around the spindle | Can show small errors, but needs a suitable holder and careful setup. |
For most woodworkers, a verified square is the sensible starting point. A dial indicator is useful when you need to diagnose a table that will not adjust evenly, but it is easy to get a misleading reading if the indicator holder slips or the spindle has runout. Compare machinist squares if your existing square leaves uncertainty.
When the table will not align
If the table is square in one direction but not the other, first check for chips, a damaged tilt joint, or a table that is not seated against its support. Some drill presses have limited adjustment in one axis. If the manual shows a stop or set screw, adjust it only as directed; forcing the table can damage the casting or leave the lock unable to hold.
If the reading changes as you rotate the spindle, test another rod and reseat it in the chuck. Persistent movement points to a bent spindle, chuck, or quill issue. If the rod stays steady but the gap changes across the table, the table may be warped or its top may not be square to the tilt mount. A straightedge can help identify a hollow or raised area. Do not compensate for a badly warped table by tilting it until one small spot reads square; the rest of the surface will still be wrong.
Verify with a test hole
After locking the table, drill a test hole in scrap at least 1 inch thick. Use a sharp bit and a steady feed, then check the hole with a square or compare the entry and exit positions. For a more revealing test, drill through a piece of scrap and inspect whether the bit exits centered beneath the entry point. A table can pass a quick visual check yet shift under the lock or flex under pressure.
Repeat the check after changing table height, since some supports can twist slightly as they move along the column. Keep a note of the table position if you routinely use an angled setup, and recheck after tilting back to 90 degrees. For normal woodworking, a consistent square setup is more valuable than chasing fractions of a degree that your bit, stock, and feed technique cannot hold.